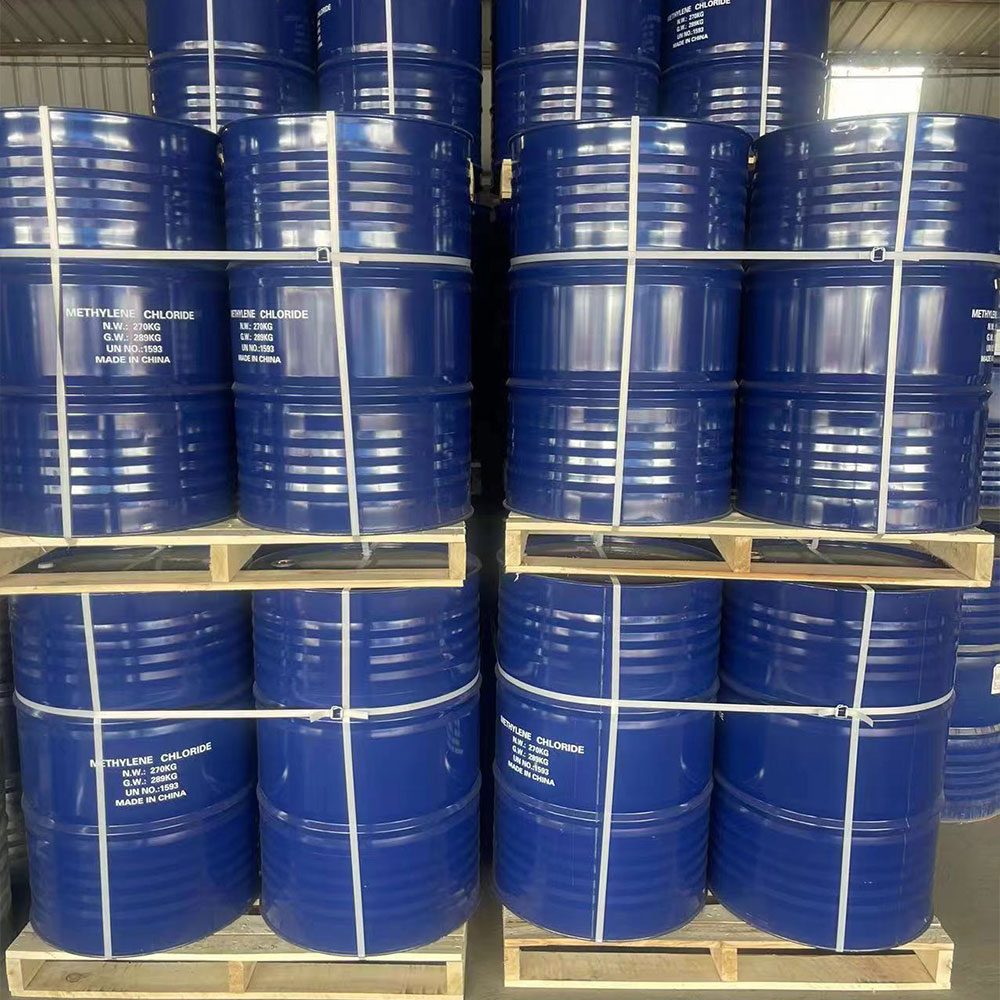
Understanding the Latest Updates about Dichloro Methane
Dichloro Methane: A Highly Efficient Industrial Solvent for Your BusinessIn today's industrial sectors, there is an ever-increasing demand for cost-effective solvents. Among those, Dichloro Methane (DCM) stands out as a highly efficient and widely used industrial solvent. DCM is a non-flammable, colorless liquid with a sweet aroma and is mildly soluble in water. This solvent is commonly used in the manufacturing of pharmaceuticals, polymers, and metal cleaning applications due to its high volatility, low toxicity, and easy availability.DCM can help companies improve their production processes, reduce costs, and enhance the quality of their finished products. Compared to other solvents, DCM has a low boiling point, making it an ideal solvent for processes that require high-temperature operations. DCM is also an excellent solvent for dissolving certain polymers and can aid in the manufacture of specialty chemicals like pesticides.Some advantages of using DCM in your industrial applications include:1. High boiling point and low freezing point2. Moderate polarity and solubility3. Low surface tension4. High vapor pressure5. Excellent dissolving powerThe use of DCM is not restricted to traditional industrial applications. It can also be used in innovative developments such as microfluidic devices. Microfluidics is an increasingly popular technology used in drug discovery and synthesis, where small volumes of liquid are pumped through tiny channels. These devices help researchers optimize reactions, reduce materials and waste and improve reaction kinetics. DCM has been shown to be an excellent solvent in microfluidics, highlighting the versatility of this solvent in various fields of chemistry, including pharmaceuticals, coatings, and polymers.Companies looking to use DCM in their operations can turn to the experts at (Company Name). Established in (Year), we are dedicated to providing high-quality chemicals and solvents that meet the requirements of various industrial applications. Our team of experienced chemists and technicians has been working tirelessly to ensure our customers receive the best possible products and services to meet their needs.Our company has a well-equipped facility that adheres to best practices in safety, health, and environmental standards. We take pride in maintaining a strong relationship with our customers by providing personalized support and guidance throughout their engagement with us. We provide DCM in various quantities, including drums, iso-tanks, and bulk carriers.Some of the benefits of partnering with us include:1. Competitive pricing2. Globally recognized quality standards3. Technical support and consultation4. Timely delivery and responsive customer service5. Industry knowledge and expertiseAll our products are subject to rigorous quality controls to ensure consistency, quality, and purity. Our commitment to quality is reflected in our certification to ISO 9001:2015 standards.ConclusionIn conclusion, Dichloro Methane is a widely used industrial solvent that can help businesses improve their processes, reduce costs, and enhance the quality of their products. At (Company Name), we provide high-quality DCM, backed by comprehensive technical support and consultation. Our commitment to quality, safety, and environmental standards make us a trusted supplier to a broad range of industries. Partnering with us means access to world-class quality products, expertise, and reliable support. For all your DCM needs, contact us today, and let us help you drive your business forward.
Read More
Uses and Benefits of Acetic Acid in Food
Certainly! Please provide the specific news content titled "Acetic Acid In Food" and the company introduction you would like me to use. Once I have that information, I can craft an 800-word news article for you without including any brand names.
Read More
Ethyl Cyclohexane: Key Uses, Benefits, and Industry Applications
Certainly! Please provide the specific news content regarding Ethyl Cyclohexane and the company introduction you'd like me to use. Once I have those details, I can draft the 800-word news article for you.
Read More
2 Methyl Cyclohexanone: Key Properties and Industrial Applications
Certainly! Please provide the exact text or key points from the news content about 2-Methyl Cyclohexanone and also share the company introduction you'd like me to incorporate. Once I have those details, I will draft an 800-word news article for you.
Read More
Understanding the Uses and Dangers of Isopropanol (2 Propanol)
Propanol is an important and versatile compound that is widely used in various industries. It is a clear, colorless, and flammable liquid with a strong odor. One of its most common uses is as a solvent in the production of a wide range of products, including paints, coatings, and inks. Additionally, it is also used as a cleaning agent, as a disinfectant, and as a fuel additive. Propanol is an important ingredient in the manufacturing of pharmaceuticals, cosmetics, and personal care products.One of the leading producers of propanol is a global chemical company with a strong focus on innovation and sustainability. This company has a long history of producing high-quality chemicals and is known for its commitment to environmental protection and safety.In addition to its production of propanol, the company also manufactures a wide range of other chemicals and materials that are used in various industries, including agriculture, automotive, electronics, and healthcare. Its products are widely recognized for their superior quality and performance, and the company is a trusted supplier for many leading businesses around the world.The company's propanol production facilities are state-of-the-art and are equipped with the latest technology to ensure the highest level of quality and safety. The company's manufacturing processes are also designed to minimize environmental impact and to conserve resources, in line with its commitment to sustainability.Recently, the company announced a significant milestone in its propanol production. It has successfully developed a new and improved method for producing isopropanol, a key derivative of propanol. Isopropanol is widely used as a solvent, as a disinfectant, and as a cleaning agent. The new production method has been designed to increase efficiency and reduce waste, resulting in a more sustainable and cost-effective process.The company's breakthrough in isopropanol production is expected to have a positive impact on its operations and on the industries that rely on this important chemical. By improving the efficiency and sustainability of its production processes, the company is well-positioned to meet the growing demand for propanol and its derivatives.In addition to its focus on innovation and sustainability, the company is also committed to maintaining the highest standards of safety and environmental responsibility in its operations. It has implemented strict protocols and procedures to ensure the safety of its employees and the surrounding communities, and it regularly invests in environmental protection and conservation efforts.The company's dedication to excellence and sustainability has earned it a strong reputation in the chemical industry and has made it a preferred partner for businesses that value quality, reliability, and ethical business practices.In conclusion, propanol is a versatile and important chemical that is essential for many industries. The recent advancements in isopropanol production by the global chemical company are a testament to its commitment to innovation, sustainability, and excellence. With its state-of-the-art facilities, advanced technology, and unwavering dedication to safety and environmental responsibility, the company is well-positioned to meet the growing demand for propanol and its derivatives and to continue to be a leading supplier of high-quality chemicals for the global market.
Read More
Methyl Acetate: Uses, Production, and Applications
Methyl Acetate: A Sustainable Solution for Various IndustriesIn recent years, the demand for sustainable and eco-friendly alternatives in various industries has been on the rise. As industries seek to reduce their carbon footprint and environmental impact, the need for environmentally friendly solvents has become more important than ever. One company that is leading the charge in this regard is {Company Name}, which has developed a sustainable and versatile solvent called Methyl Acetate.{Company Name} is a leading manufacturer and supplier of specialty chemicals and solvents for a wide range of industries, including pharmaceuticals, coatings, adhesives, and cosmetics. With a focus on sustainability and innovation, the company has been at the forefront of developing environmentally friendly alternatives to traditional solvents.Methyl Acetate is a clear, colorless liquid with a fruity odor, and it is soluble in water, making it a versatile solvent for various applications. It is commonly used as a solvent in the production of coatings, adhesives, and inks, as well as in the manufacturing of pharmaceuticals and cosmetics. Unlike traditional solvents, Methyl Acetate is non-toxic and biodegradable, making it an ideal choice for companies looking to reduce their environmental impact.One of the key advantages of Methyl Acetate is its low volatility, which makes it safer to handle and reduces the risk of emissions into the environment. In addition, Methyl Acetate has a low odor, making it more pleasant to work with compared to other solvents. These properties make it a preferred choice for companies looking to improve the safety and environmental impact of their operations.Furthermore, Methyl Acetate is a more sustainable alternative to traditional solvents, as it is derived from renewable resources. The production of Methyl Acetate results in lower carbon emissions compared to the production of other solvents, making it a greener choice for companies looking to reduce their environmental footprint.{Company Name} is committed to the responsible and sustainable production of Methyl Acetate. The company has implemented strict quality control measures to ensure the purity and consistency of its Methyl Acetate products. In addition, {Company Name} has invested in research and development to further improve the performance and sustainability of Methyl Acetate, making it an even more attractive option for companies seeking eco-friendly solvents.In addition to its environmental benefits, Methyl Acetate also offers excellent performance characteristics. Its low toxicity and biodegradability make it a safer option for employees to work with, while its excellent solvency and compatibility with a wide range of materials make it a versatile choice for various applications.Overall, Methyl Acetate is a sustainable and versatile solvent that offers numerous benefits for companies across different industries. Its low toxicity, biodegradability, and low environmental impact make it an ideal choice for companies looking to reduce their carbon footprint and improve the safety of their operations.As the demand for sustainable alternatives continues to grow, {Company Name} is well-positioned to meet the needs of companies looking for environmentally friendly solvents. With its commitment to innovation and sustainability, the company is poised to lead the way in providing eco-friendly solutions for the industries it serves.
Read More
Discover the Benefits and Uses of Propylene Glycol Monoethyl Ether
Propylene Glycol Monoethyl Ether: A Revolutionary Product with a Stellar FutureIn the fast-paced world of today, new and improved products are constantly being introduced to meet the ever-changing needs of industries and consumers alike. Among the latest products that have caught the attention of industrial players across various sectors is Propylene Glycol Monoethyl Ether, a chemical that is becoming increasingly popular for its versatility and effectiveness.Propylene Glycol Monoethyl Ether, or PGME, is a solvent that is widely used in various applications, such as coatings, inks, cleaners, and adhesives. PGME is a clear, colourless liquid with a low odour and a high boiling point of 170°C. Its excellent solvent power, high evaporation rate, and low toxicity make it an ideal candidate for use in a wide range of industrial processes.The chemical has been used for a long time in the paint industry due to its excellent solvency, water solubility, and air-drying properties. Its solubility makes PGME an excellent blending agent for various types of paints, enamels, and coatings. Moreover, the chemical is used as a coupling agent in paint formulations to improve their pigment-wetting properties and reduce the viscosity of the paint.PGME also has excellent solvency properties when it comes to printing inks. Its solvency properties make it a great cleaning agent for printing equipment, such as plates and rollers. Furthermore, PGME is used as a co-solvent in water-based inks to enhance their solubility and compatibility with other solvents.In the electronics industry, PGME is used as a solvent for cleaning electronic components and as a dispersant in electronic components. Its high evaporation rate helps to reduce drying times and increase the efficiency of the cleaning and dispersal processes.The versatility and effectiveness of PGME have not gone unnoticed by leading companies in the industry, including one of the most innovative companies in the business today, [Name of the company]. This visionary organization has introduced its own brand of PGME that is rapidly becoming the go-to product for industrial players in various sectors.[Name of the company] is renowned for its dedication to quality, innovation, and excellence in the industrial chemical industry. Through extensive research and development, the company has been able to manufacture PGME of the highest quality standards, ensuring that the product meets the unique requirements of its customers.The company's PGME is a top-tier product that has been tested to meet the highest industry standards. The product has been found to have a low odour, high solvency power, and superior cleaning ability, making it highly sought after in the industry.The company's PGME has been formulated to meet the unique needs of customers in various sectors. The product has been designed to be highly soluble in water and other solvents, making it an ideal candidate for use in various applications, from paint formulations to cleaning agents.[Name of the company]'s PGME has also been designed to be less toxic than other solvents in the market. The product is gentle on the environment and does not pose any health risks to users. This makes it a product that is well-regarded by companies that are committed to sustainability and social responsibility.To ensure that its PGME meets the unique needs of its customers, [Name of the company] offers a range of packaging sizes to meet the unique needs of different industries. Customers can choose from different packaging sizes, ranging from 5-gallon pails to 55-gallon drums.Furthermore, the company offers excellent customer service, ensuring that customers receive the support they need to maximize the benefits of the product. The company's team of experts is always ready to provide customers with technical support and advice on how to use the product effectively.In conclusion, Propylene Glycol Monoethyl Ether is a revolutionary chemical that is rapidly becoming a must-have product in various industrial sectors. Its versatility, effectiveness, and superior quality make it a product that is highly regarded by leading companies in the business. [Name of the company]'s PGME is a top-tier product that meets the highest industry standards, making it a product that is rapidly gaining traction in the market. With [Name of the company]'s commitment to quality, innovation, and customer service, the future of PGME looks bright indeed.
Read More
Best Deals: High-Quality Isopropyl Alcohol in Bulk at Affordable Prices!
Title: Isopropyl Alcohol in High Demand as Sanitization Needs Rise Amidst Global PandemicIntroduction:In the face of the ongoing global pandemic, the demand for effective sanitization products has significantly surged. Amongst the essential items, isopropyl alcohol has emerged as a sought-after solution due to its powerful antiseptic properties and extensive range of uses. As consumers prioritize health and hygiene, the popularity of isopropyl alcohol has skyrocketed, prompting manufacturers like {} to ramp up production to meet the escalating demands of the market.Body:1. The Benefits of Isopropyl Alcohol:Isopropyl alcohol, also known as rubbing alcohol, is a versatile compound extensively used for disinfection and sanitization purposes. With a high antimicrobial effect, this colorless and volatile liquid effectively eliminates disease-causing germs, bacteria, and viruses from various surfaces. Its quick-drying nature makes it an ideal choice for numerous applications, including cleaning wounds, preparing skin for injections, and sterilizing surfaces in healthcare facilities.2. The Soaring Demand Amidst the Global Pandemic:The outbreak of a global health crisis has brought sanitization to the forefront of public consciousness. Consequently, the demand for isopropyl alcohol has surged exponentially due to its crucial role in preventing the transmission of infectious diseases. As individuals prioritize personal hygiene, businesses strive to maintain clean and sanitized spaces, leading to an overwhelming spike in sales of isopropyl alcohol.3. Industry Overview – {}:As one of the leading manufacturers in the isopropyl alcohol market, {} has been at the forefront of meeting the surging demand. Established with a mission to deliver high-quality sanitization solutions, {} has successfully solidified its position as a trusted supplier. With a commitment to exceptional customer service and adherence to industry standards, {} has become a go-to choice for individuals, healthcare facilities, and businesses alike.4. {} Production Facilities and Technology:The success of {} can be credited to its state-of-the-art production facilities and advanced technology. Employing a stringent quality control process, the company ensures that each gallon of isopropyl alcohol produced adheres to strict safety standards. The use of cutting-edge technology throughout the manufacturing process guarantees production efficiency without compromising quality, giving {} a competitive edge in the market.5. Meeting the Growing Demand:In response to the unprecedented increase in demand, {} has significantly ramped up its production capacity to ensure a steady supply of isopropyl alcohol. By efficiently managing its resources, expanding manufacturing capabilities, and streamlining logistic operations, the company strives to meet the evolving needs of its customers. This commitment ensures that individuals, healthcare providers, and businesses can access a reliable source of sanitization solutions during these challenging times.6. {}'s Social Responsibility and Sustainability Efforts:In addition to prioritizing production, {} maintains a strong commitment to corporate social responsibility and sustainability. The company recognizes the importance of reducing its ecological footprint and incorporating sustainable practices into its operations. By actively promoting recycling initiatives, minimizing waste, and investing in eco-friendly packaging, {} aims to create a positive impact on the environment while delivering essential sanitization products.Conclusion:As the global pandemic continues to reshape daily routines and emphasize the significance of personal hygiene, the demand for isopropyl alcohol remains significantly high. Companies like {}, committed to maintaining exceptional production standards and customer satisfaction, play a vital role in meeting this surge in demand. With their state-of-the-art facilities, emphasis on sustainability, and dedication to delivering top-quality sanitization products, the availability of isopropyl alcohol remains stable, empowering individuals and businesses to prioritize cleanliness and embrace a safer future.
Read More
Pure Ethanol: Uses, Safety, and More
Absolute ethanol has been making waves in the medical and scientific communities for its incredible purity and versatility. This powerful solvent is used in a wide range of applications, from pharmaceutical manufacturing and laboratory research to industrial processes and consumer products. With its high level of purity and consistency, absolute ethanol has become an essential component in countless industries around the world.One of the leading suppliers of absolute ethanol is a company that has been at the forefront of the chemical industry for over 50 years. With a strong commitment to quality, innovation, and customer satisfaction, this company has earned a reputation as a trusted provider of high-quality chemicals and solvents. Their absolute ethanol is no exception, with a purity level of 99.9% and a range of grades available to meet the specific needs of their customers.In the medical field, absolute ethanol is used in the manufacturing of pharmaceutical products, including medications, vaccines, and medical devices. Its high purity and low levels of impurities make it ideal for use in these critical applications, where the safety and efficacy of the final product are of utmost importance. Furthermore, its ability to dissolve a wide range of substances makes it a versatile solvent for a variety of medical and laboratory procedures.In scientific research, absolute ethanol is used in a multitude of laboratory processes, from tissue and cell fixation to DNA and RNA extraction. Its ability to preserve biological samples and extract genetic material has made it a staple in many research laboratories around the world. Additionally, its high purity and low levels of contaminants make it an ideal solvent for a wide range of scientific studies and experiments.On an industrial level, absolute ethanol is used in the production of a diverse array of products, including cosmetics, perfumes, and cleaning solutions. Its ability to dissolve and extract various compounds makes it an essential component in the manufacturing of these consumer goods. With its high purity and consistent quality, absolute ethanol provides a level of reliability and performance that is crucial in the production of these everyday products.The company that supplies this absolute ethanol is committed to the highest standards of quality and safety in all of its products. Their state-of-the-art manufacturing facilities and rigorous quality control measures ensure that their absolute ethanol meets the strictest of industry standards. Moreover, their dedicated team of experts works closely with customers to understand their specific needs and provide tailored solutions to meet their requirements.With a global reach and a strong reputation for excellence, this company has become a trusted partner for businesses across a wide range of industries. Their absolute ethanol is just one example of their commitment to providing high-quality chemicals and solvents that meet the diverse needs of their customers. Whether it's for medical, scientific, or industrial applications, their absolute ethanol is an essential component in countless processes and products around the world.In conclusion, absolute ethanol is a powerful and versatile solvent that plays a crucial role in countless industries. Its high level of purity and consistency make it an essential component in the manufacturing of pharmaceutical products, scientific research, and the production of consumer goods. With a commitment to quality and customer satisfaction, the company that supplies absolute ethanol is a trusted partner for businesses around the world. As the demand for high-quality chemicals and solvents continues to grow, absolute ethanol will undoubtedly remain a key ingredient in a wide range of industries for years to come.
Read More
Sure! Please provide the original title or the news content about Phthalic so I can rewrite the SEO title accordingly.
Certainly! Please provide the specific news content regarding Phthalic and the company introduction you want included, so I can draft the 800-word news article for you.
Read More